YOUR CART
- No products in the cart.
There exists a misconception on testing requirements for vacuum impregnation sealants and vacuum impregnation processes. Testing impregnation sealants for application compatibility and testing the impregnation process effectiveness are grossly different.
In 2008, a North American motorcycle OEM decided to insource their vacuum impregnation requirements to reduce manufacturing costs. The OEM considered multiple sealant and equipment technologies. The company was sold on equipment that claimed to eliminate wastewater discharge, seal castings at a better rate, and would require minimal adjustments, maintenance, and repair. The equipment selected used a recycling sealant.
(more…)
The Continuous Advanced Powertrain Impregnation system (CAPI) allows high volume OEM and suppliers to have the benefits of vacuum impregnation in a simple, easy to use machine. In our latest video, Johnny Impreg discusses how the system effectively seals die casting leak paths while eliminating contamination and damage.
Automotive manufacturers realize that being environmentally responsible and profitable are not mutually exclusive. Being environmentally responsible can achieve better growth, cost savings, improve brand recognition, and increase profitability. The environmental impact of the responsible use of resources is beneficial to everyone, and automotive manufacturers play a leading role.
Back by popular demand, John Halladay (aka Johnny Impreg) shows our latest vacuum impregnation system, the Advanced Powertrain Impregnation system (APi). The APi allows powertrain manufacturers to have the benefits of vacuum impregnation in a simple, easy to use machine.
The ISM Manufacturing Index measures manufacturing activity based on a monthly survey of more than 300 manufacturing purchasing managers. The survey is conducted by the Institute of Supply Chain Management (ISM).
(more…)
In its latest analysis, IHS Markit has revised its global light vehicle sales and production forecasts due to the COVID-19 impact. IHS Markit’s latest study now projects light vehicle sales to be 69.6 million units, while production is predicted to fall to 69.3 million units.
(more…)
Waste is any activity that consumes resources but brings no product value. Eliminating non-value, unnecessary waste is crucial for a company’s success. If not removed, waste can lower profitability, increase costs, decrease quality, and lower employee satisfaction.
Like most manufacturing processes, porosity is inherent to powder metallurgy. Porosity is only considered a defect if it is interconnected and creates a leak path can affect the part’s structural integrity and performance. This blog discusses the four main reasons why vacuum impregnation is used to seal powder metallurgy leak paths.
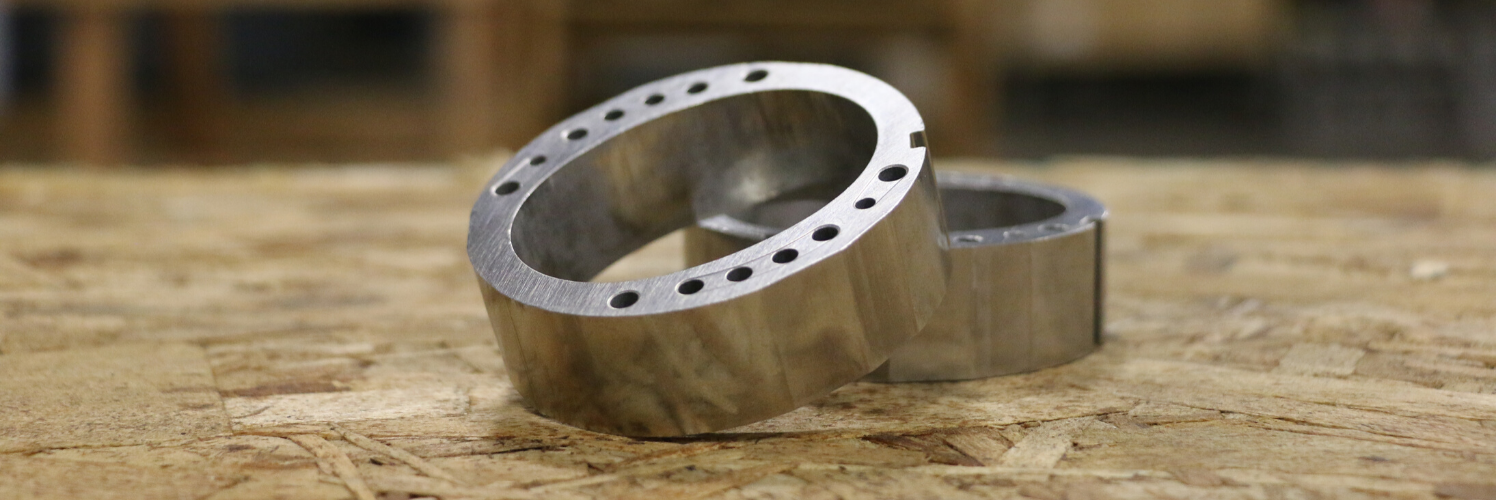
If the leak paths are not sealed, then fluids or gases may leak from the part. Vacuum impregnation prevents fluids or gases from leaking by sealing the porosity and leak paths. The process does this without changing the powder metal component’s dimensional or functional characteristics
Plating operations submerge the parts in acid solutions. The residual acid can seep into the porosity, which causes corrosion. Sealing the components before plating eliminates the risk of internal corrosion.
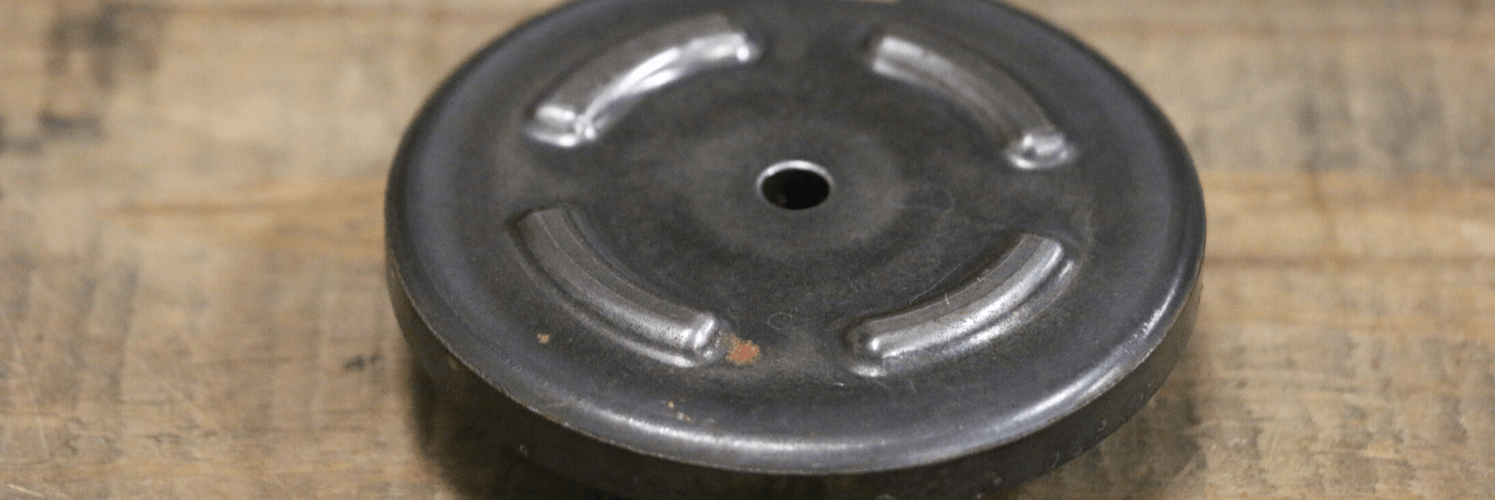
Secondary machine operations, such as drilling, tapping, or cutting, are impaired as the voids between the particles cause tool chatter, reducing tool life and finish quality. Vacuum impregnation stabilizes and supports the individual powdered metal granules during machining. This improves machinability by making it more efficient, eliminating tool chatter, and improving the machined finish.
Powder metal porosity absorbs oils, fluids, deburring fluids, pre-plating cleaners, and acids. If not sealed, fluids may bleed out and negatively affect the finish. Sealing the porosity before secondary finishes will eliminate any failure mode that could develop from bleed out of pretreatments.
Vacuum impregnation adds value to powdered metal components. The process eliminates failure modes caused by porosity, produces pressure tight parts, improves machinability, and meets surface finish/appearance requirements.
An effective production flow involves work stations and equipment to be arranged in a sequence that supports a smooth flow of parts and materials with minimal delays. Implementing an efficient production flow leads to increased production and flexibility, as well as a reduction in capital requirements.
Anoplate, an industry leader in surface engineering, faced a production flow dilemma. The company offers vacuum impregnation services to seal leak paths and eliminate failure modes that could develop from outgassing, chemical compatibility, or bleed out of pretreatments in porous materials. Anoplate processes high value, complex die castings for some of the largest and most respected aerospace, defense, information technology, and recreation companies in the world. The castings often have thin walls with small blind taps.
The Challenge
Anoplate’s operations span across two buildings. Its headquarters comprises of its offices and vacuum impregnation operation. The second building, located across the street, houses its vapor degreasing and plating operations. Anoplate uses in-house batch impregnation systems to process the die castings. The batch system aggregates various parts and processes them in large batches. Before impregnation, parts are processed through vapor degreasing.
Despite being well versed in vacuum impregnation, the company could not efficiently process complex castings due to three limitations of their batch systems.
The SolutionThe company laid out its vision, and Godfrey & Wing responded with the lean, front-loading HVLV vacuum impregnation system, customized to address the company’s challenges.
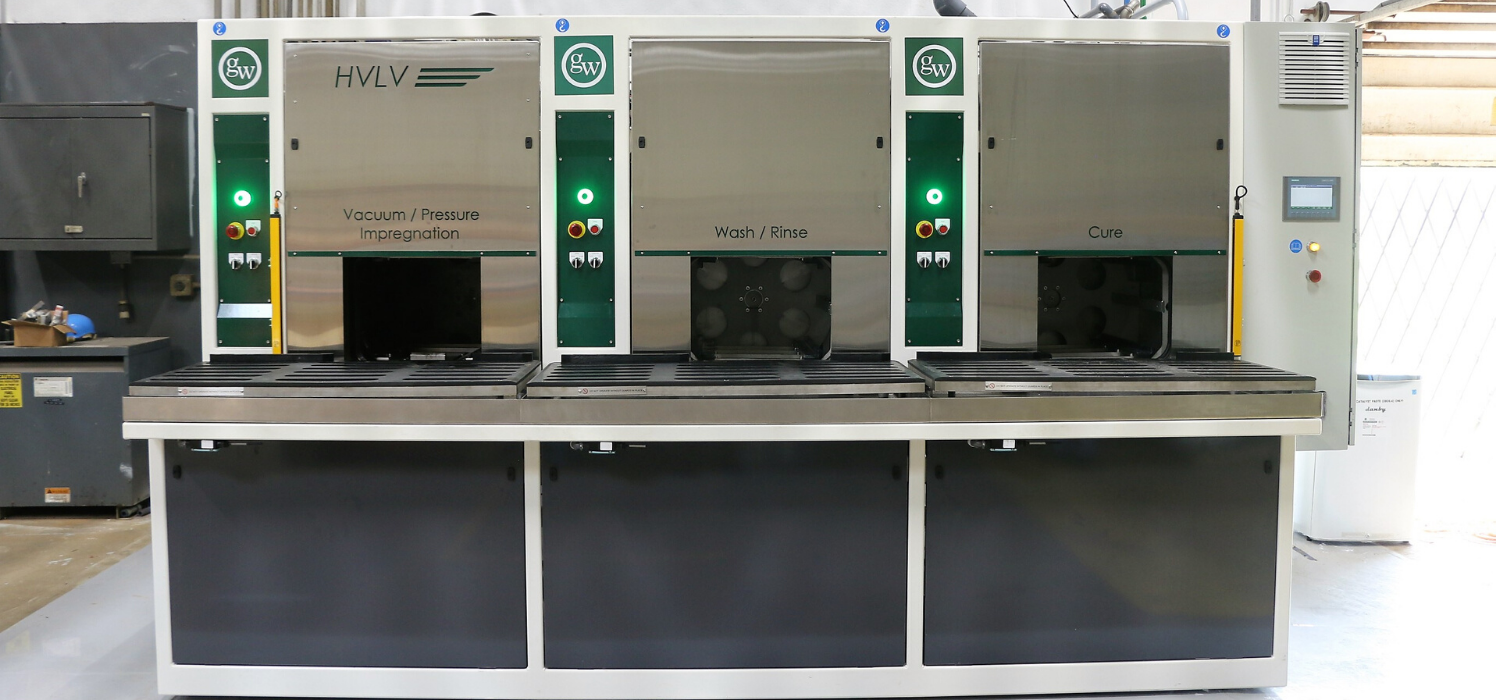
To eliminate contamination, Godfrey & Wing designed custom fixtures to maximize the number of castings per cycle and protect critical machined features. The HVLV’s advanced wash cycle was programmed with an aggressive wash to flush sealant from blind holes and machine features.
After impregnation, the part is centrifuged to recover unused sealant. The sealant is returned to the sealant reservoir for use in subsequent cycles. The HVLV recovers unused sealant before the wash, which eliminates sealant drag out, and risk of contamination.
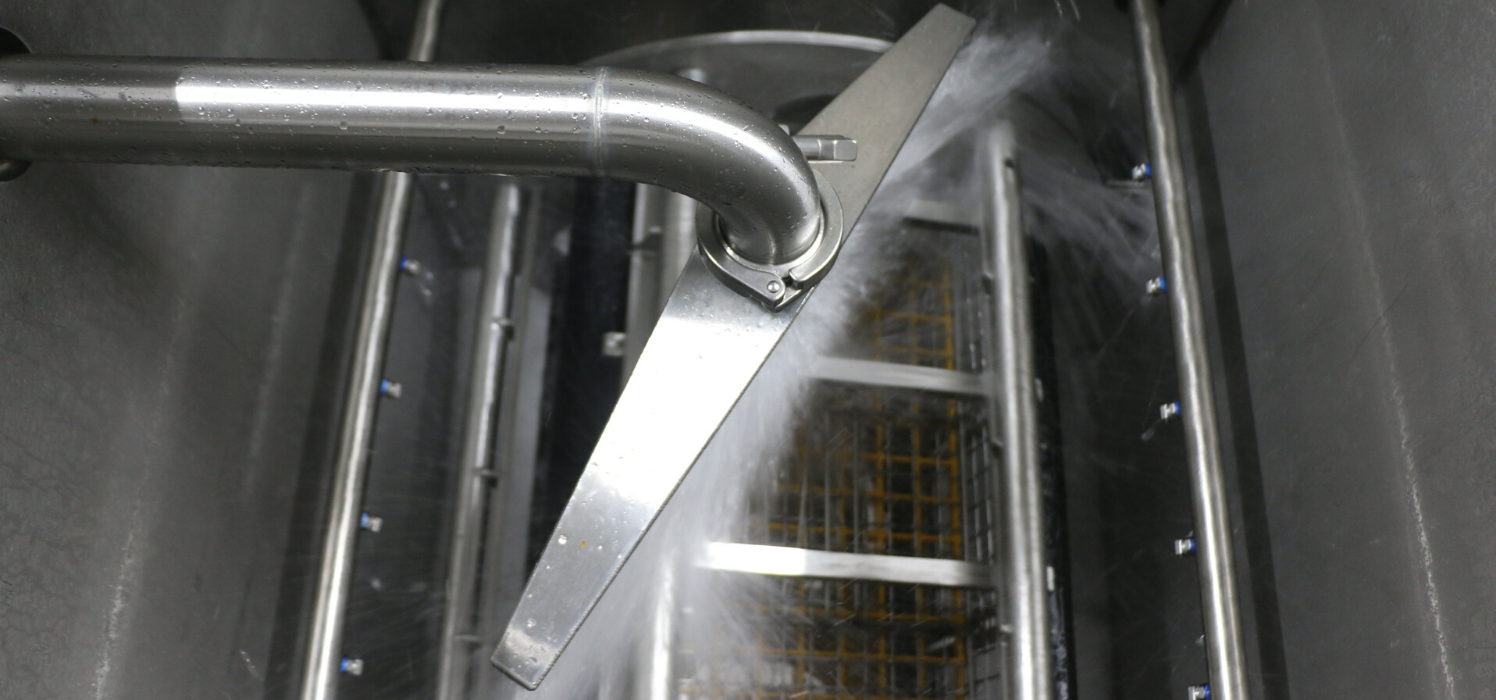
Recognizing the company’s desire to place the system in the same building as plating, Godfrey & Wing designed the HVLV to align with production. HVLV’s modular footprint requires 96 square feet without any floor changes. Godfrey & Wing also studied how the HVLV would integrate with Anoplate’s order of operations and concluded that with the HVLV, Anoplate’s vapor degreasing process could be eliminated.
While the system sounded perfect, Anoplate conducted rigorous sample testing before investing. Samples were processed at Godfrey & Wing’s headquarters on a machine identical to the HVLV proposed to Anoplate. The results demonstrated that the HVLV not only sealed the leak paths, but eliminated contamination, and reduced sealant usage. Also, the company was able to see firsthand how the modular footprint could easily fit into its existing production line. With these results, Anoplate purchased an HVLV.
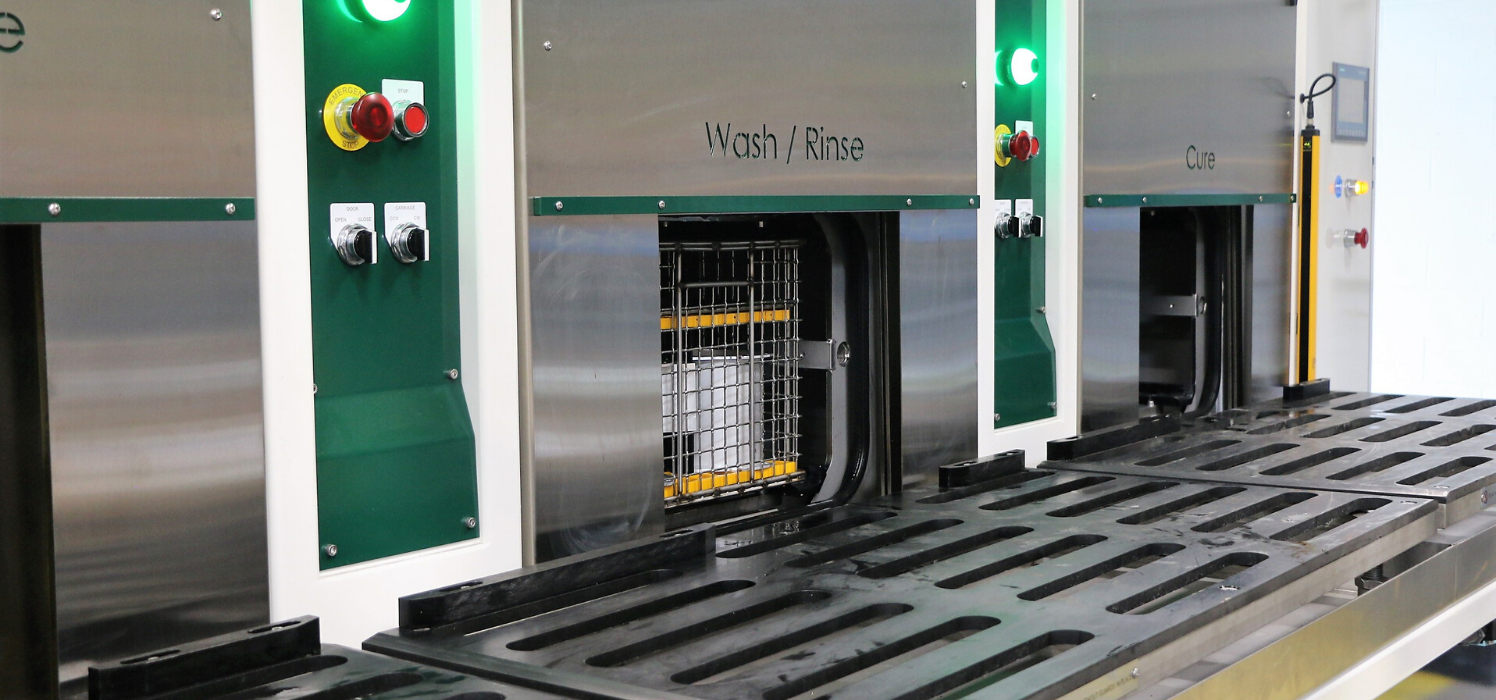
The Results
The HVLV was installed, operators and maintenance were trained, and the system was processing parts in under two weeks. Since then, the HVLV is addressing Anoplate’s challenges.
“Considering our challenges, the HVLV has been a very effective solution delivering unrivaled quality for our advanced manufacturing environment.” Said Jesse Campbell, Anoplate’s Vice President of Engineering, “This system has also changed our perception of vacuum impregnation equipment in that it is simple to use, and the look is sleek and modern.”
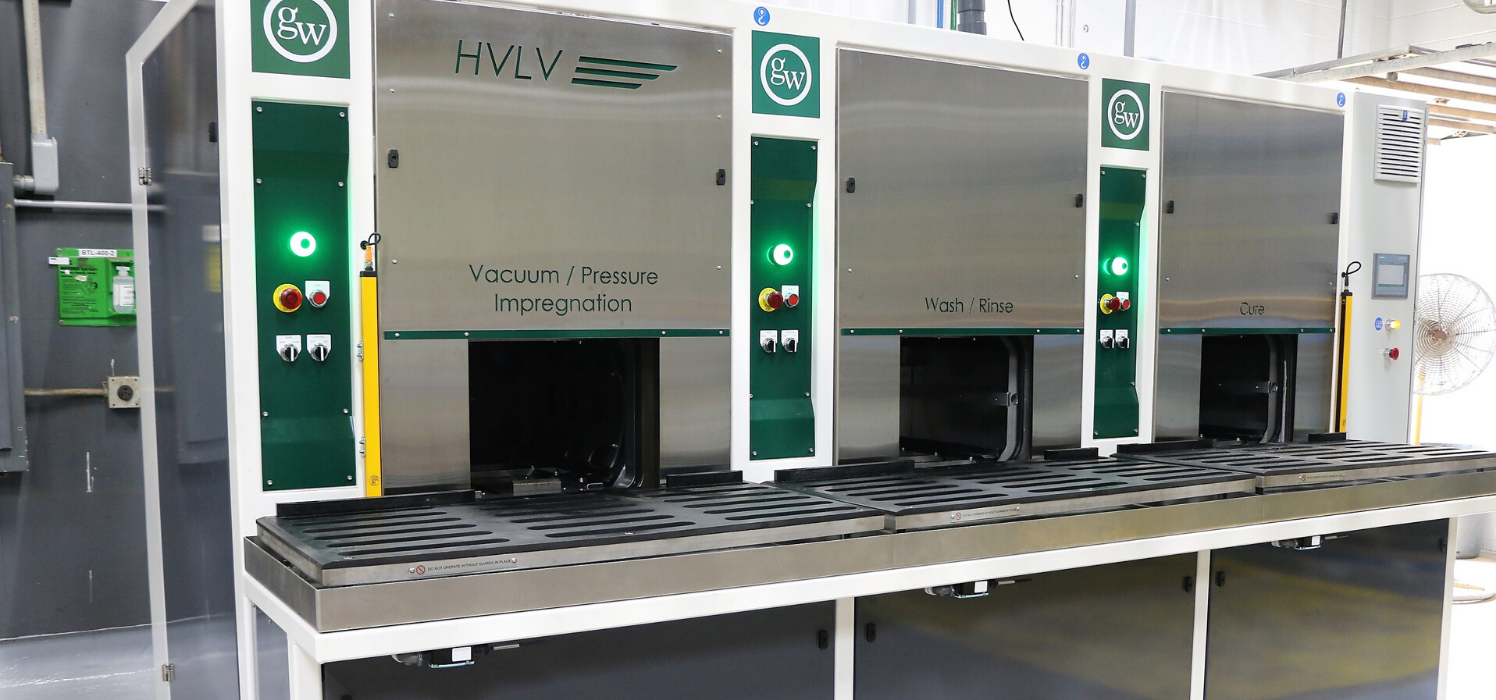
In SummaryThe HVLV has created a competitive advantage to Anoplate’s vacuum impregnation services. The system has transformed its impregnation business by reducing costs, increasing quality and improving efficiency.