YOUR CART
- No products in the cart.
At Imprex, a division of Godfrey & Wing, we’ve built something new for engineers who want a clearer picture of how vacuum pressure impregnation works: an interactive infographic that walks through each stage of the VPI process.
Engineers evaluating insulation methods or designing new winding systems will find a visual, hands-on way to understand the technology behind high-performance insulation. Below, learn more about the importance of VPI process technology, the sequence it follows, and how our new interactive infographic visualizes the process step-by-step.
Motors, generators, and transformer windings are expected to operate under continual stress, withstanding heat, vibration, contamination, and more. Standard methods like varnish dipping often leave air pockets and voids in the winding structure that can lead to premature wear or failure.
The vacuum pressure impregnation process eliminates voids by forcing insulating resin deep into the winding under controlled vacuum and pressure conditions. The result is a fully saturated, bonded insulation system that holds up where conventional treatments fall short.
Several outcomes engineers rely on VPI technology to achieve include:
For OEM designers and motor rebuilders, these variables can affect service life, reliability ratings, and other bottom-line requirements.
The vacuum impregnation process follows a precise sequence. Each stage depends on the one before it. Skip a step or rush through it, and the final insulation quality suffers.
The first step involves preheating the part in an oven to drive out residual moisture and bring the winding to the right temperature for resin absorption. The part then goes into the pressure vessel, and the chamber is sealed. A vacuum is pulled until air is fully evacuated or a pre-specified vacuum level is reached.
With the vacuum still applied, the transfer valve opens and resin flows into the impregnation chamber. The part sits submerged in resin while under vacuum, with no air left to block absorption. Pressure is then applied to drive the resin into every remaining void. This deeper, thorough penetration is what separates VPI from simple dip-and-bake methods.
Unused resin returns to the holding tank, and the impregnated part goes back into the oven. Heat cures the resin, locking the insulation system in place.
Our new interactive infographic is a step-by-step visual guide for engineers who need more than a text description. Move through each stage at your own pace, with visuals showing what’s happening inside the pressure vessel at every step. The dry vacuum phase, the resin fill, the pressure application, and the cure cycle are presented as a connected, logical sequence, showing how process control and resin chemistry come together through VPI technology to improve heat dissipation in parts and create a solid, completely sealed structure.
The vacuum pressure impregnation process makes transformers, motors, and other components better at resisting electrical breakdowns, withstanding harsh operating conditions, and performing optimally over longer periods.
Hover over the pulsing buttons in each step to learn more about each stage.
Industrial automation, EV propulsion, and heavy electrical manufacturing demand high-performance stator assemblies that withstand severe thermal stress, moisture, and continuous electrical loads. At Imprex, a division of Godfrey & Wing, we design advanced vacuum impregnation equipment, sealants, and automated processing systems engineered to preserve structural integrity across critical components. Learn more about evaluating electric motor winding insulation strategies, comparing secondary insulation processes, and choosing modern motor insulation materials to enhance long-term operational efficiency.
Protecting copper conductors against turn-to-turn short circuits requires applying robust primary and secondary insulation layers. Manufacturers rely on several primary motor insulation materials and processing methods depending on production volume and performance criteria:
Traditional dip-and-bake methods rely on gravity and capillary action to draw resin into winding bundles. This approach can trap air pockets rather than allowing for full displacement.
Vacuum Pressure Impregnation (VPI) eliminates air entrapment. The dry vacuum cycle evacuates moisture and air from the winding matrix before introducing solventless resin. Positive pressure then forces liquid resin deep into microscopic voids. This thorough saturation establishes a tight electric motor seal throughout the stator core to provide a solid, void-free structure.
VPI processing results in thorough saturation and airtight sealing throughout the entire structure. Eliminating internal air gaps provides essential motor winding protection against moisture, abrasive dust, and aggressive chemical vapors, with benefits that include:
Our VPI technology creates a reliable electric motor seal around complex winding geometries. This complete motor winding sealing reduces stress on internal components during frequent start-stop cycles, supporting a longer service life.
Evaluating manufacturing techniques involves gauging processes against field reliability:
| Performance Attribute | Dip & Bake Varnish | Trickle Resins | Vacuum Pressure Impregnation (VPI) |
| Void Elimination | Low (air pockets can remain) | Moderate | Complete evacuation |
| Heat Dissipation | Poor thermal transfer | Moderate | High thermal conductivity |
| Field Life Expectancy | Standard | Extended | High reliability under stress |
VPI processing with advanced electric motor insulation materials allows for complete coverage, improved heat dissipation, and high reliability in the field. To explore our full engineering capabilities, equipment designs, and processing sealants, visit the official Godfrey & Wing homepage.
Achieving consistent void-free impregnation requires precise process control and chemistry. At Imprex, we provide turnkey vacuum impregnation systems with high-efficiency tailored to modern manufacturing demands. Upgrading a stator insulation line with our automated systems can protect windings while maintaining strict quality standards across runs.
Contact our team today to consult with an impregnation engineer about your manufacturing requirements.
Modern EV architectures, industrial automation, and high-reliability aerospace assemblies depend on delicate circuitry that must operate flawlessly under aggressive moisture exposure and severe vibration. At Godfrey & Wing, we manufacture advanced vacuum impregnation equipment, specialized resin sealants, and processing lines engineered to seal internal voids across sensitive electronic applications. Learn more about the advantages of vacuum impregnation for electronics and how to implement effective strategies for sealing electronic components against environmental degradation.
The vacuum impregnation process seals internal air gaps, micro-porosities, and leak paths within electrical connectors, sensors, and power distribution modules. The process begins by pulling a deep vacuum to evacuate trapped air from internal voids.
Once evacuated, liquid resin enters the chamber and penetrates microscopic voids. Positive pressure then drives the sealant deep into every internal cavity. Excess resin washes away from external surfaces before curing transforms liquid sealant into a permanent polymer barrier. Using vacuum impregnation with electronics establishes an internal seal without altering external dimensional tolerances or adding excess assembly weight.
Unsealed micro-porosities in cast housings, overmolded connectors, and terminal pins act as pathways for moisture, dust, and corrosive fluids. This can compromise the insulation’s electrical resistance. Uncontrolled moisture migration can also lead to oxidation in battery terminals and power modules.
Preventing battery corrosion in electronics means using the right method to effectively seal leak pathways before fluid reaches active circuits. Thoroughly sealing electronic components preserves system integrity in the given operating environment.
Vacuum impregnation technology is used to seal electronics for several key reasons, including its ability to effectively seal leak paths, shield internal parts against moisture, and meet quality demands.
Overmolded parts and electrical winding systems can develop microscopic air gaps during cooling due to differing thermal expansion rates. Applying vacuum impregnation completely seals hidden leak paths to create a solid, uniform mass.
Moisture that migrates through voids can accelerate wear and lead to premature failure in electronics. The vacuum impregnation process seals these voids to shield internal contacts from harsh automotive fluids, chemicals, and humidity.
Traditional insulation methods can add bulk to electronics or restrict compact layout designs. Utilizing a precise vacuum impregnation process provides robust environmental protection to seal internal leak paths without compromising on weight or space constraints, allowing engineers to maintain dimensional and layout requirements.
Using vacuum impregnation supports effective sealing and reliability across critical electronics applications. Examples of its use cases and benefits are shown below:
| Application / Component | Primary Failure Mode Addressed | Core Benefit of Vacuum Impregnation |
| Wire/Wire Harnesses | Voids between stranded wires | Seals leak paths |
| Overmolded Connectors | Pin-to-plastic leak paths | sealing the pin-to-plastic leak path |
| Power Inverters | Thermal shock & condensation | Enhances dielectric isolation and heat transfer |
| EV Battery Enclosures | Fluid/coolant leakage and moisture ingress | Seals leak paths to prevent fluid ingress |
Advanced vacuum impregnation techniques like single-point impregnation can be used with specific sealants to fill air gaps without exposing sensitive components to full immersion.
At Godfrey & Wing, our team provides vacuum impregnation equipment and high-performance resin chemistries tailored to modern electronics manufacturing. Our vacuum impregnation systems integrate directly into assembly lines, delivering rapid cycle times and dependable processing.
Contact our team today via our contact page to consult with an impregnation specialist about your specific application.
A casting that fails a leak test after machining represents far more than the loss of the raw casting. By that point, the manufacturer may have already invested in heat treatment, CNC machining, washing, inspection, material handling, and valuable production capacity.
Porosity is inherent in many metal casting processes. The manufacturing challenge is not just eliminating every microscopic void, but also preventing interconnected porosity from becoming a leak path that allows air, gas, coolant, oil, or other fluids to pass through the finished component.
Vacuum impregnation permanently seals these internal leak paths. When properly engineered into the manufacturing process, it can reduce scrap, recover otherwise usable components, stabilize leak-test performance, and protect production throughput.
Porosity can develop during solidification as a result of trapped gas, shrinkage, oxide films, inclusions, or other casting-process variables. Some voids remain isolated within the casting and never affect part performance. Others connect and form a continuous leak path through the component wall.
These leak paths may not become apparent until after machining removes the casting skin and exposes the internal porosity. As a result, a part can pass through several value-added manufacturing operations before failing a pressure or leak test.
The cost of that failure can include:
For high-volume manufacturing operations, even a relatively small porosity-related rejection rate can lead to significant cost and capacity losses, making effective porosity sealing and manufacturing defect reduction critical.
Vacuum impregnation does not remove porosity or change the casting. It fills and permanently seals interconnected porosity that would otherwise allow fluids or gases to pass through the component.
During the impregnation process, air is evacuated from the internal leak paths under vacuum. A low-viscosity liquid sealant is then introduced and driven into the porosity using a controlled combination of vacuum and pressure. Excess sealant is removed from the part surface, and the sealant remaining inside the leak paths is cured to form a permanent internal seal.
Because the sealant is contained within the porosity, the process does not alter critical part dimensions or the functional characteristics of the casting.
Vacuum impregnation allows manufacturers to retain the value from a casting rather than scrapping the component after a leak-test failure.
A properly designed process can provide several manufacturing benefits:
Vacuum impregnation is sometimes viewed solely as a method for salvaging rejected castings. In many modern manufacturing programs, however, it is designed into the production process from the beginning. Manufacturers may use vacuum impregnation in several ways:
The correct strategy depends on the component, casting process, leak specification, production volume, cost of failure, and quality requirements.
Effective vacuum impregnation requires more than placing a casting into a vacuum chamber. The complete process must be engineered around the application. Important factors include:
A process that performs well for one component may not be appropriate for another. Equipment configuration, sealant chemistry, cycle parameters, wash effectiveness, and cure performance must work together to produce a consistent result.
Godfrey & Wing engineers complete vacuum impregnation solutions for manufacturers that need to control leaks caused by casting porosity. Our capabilities include:
By combining equipment, sealant, automation, and process expertise, Godfrey & Wing helps manufacturers integrate porosity sealing as a controlled aspect of the production process rather than an unpredictable source of scrap.
Contact Godfrey & Wing to discuss your casting and production requirements or existing impregnation process.
Today’s electric motors generate significant amounts of heat from resistance and friction and must effectively handle thermal and electric stress. The performance of electric motor insulation is central to this. When insulation degrades, equipment issues or breakdowns can follow and result in production downtime.
For electrical engineers and motor designers, selecting high-quality electric motor insulation materials is just one part of the equation. The process used to apply these materials can also impact the long-term reliability of electric motors. To achieve peak efficiency and prevent premature failure, manufacturers increasingly rely on vacuum pressure impregnation (VPI) technology. Learn more about electric motor insulation performance and how VPI elevates equipment reliability.
Electrical machine windings can experience mechanical, thermal, and environmental stress during standard operation. Over time, these harsh conditions can degrade the electric motor insulation, causing sudden electrical breakdowns. A common culprit behind insulation failure is microscopic air gaps that become trapped within insulation layers.
Air pockets can localize electrical stress, which can degrade motor insulation materials over time. Furthermore, untreated air gaps can allow moisture infiltration and chemical contamination to bypass unsealed areas. Continuous start-and-stop cycles can also generate aggressive physical vibrations that can lead to faster wear.
Vacuum pressure impregnation resolves these vulnerabilities by removing trapped air and moisture and then filling air pockets. The component goes into a sealed pressure vessel where a deep vacuum extracts air and moisture from the micro-voids. While maintaining the deep vacuum, protective resin or varnish is drawn into the chamber.
The system releases the vacuum and applies positive overpressure, forcing the liquid resin deep into the tightest spaces of the electric motor winding insulation. The elimination of internal air gaps helps keep heat from concentrating in critical hot spots and locks wires into a solid protected structure.
Implementing VPI directly optimizes the mechanical strength and electrical performance of industrial machinery. By establishing a bond across electric motor winding insulation layers, this technology eliminates core mechanisms of insulation failure.
Keeping the operating temperatures low prevents thermal degradation and maintains steady dielectric performance across variable loads. Additionally, total encapsulation creates an airtight shield against corrosive chemicals and moisture. The cured resin also prevents abrasion and reduces the impact of vibration on critical components.
Achieving exceptional electric motor insulation requires matching advanced VPI technology with the appropriate resins. Manufacturers must evaluate the specific thermal classifications and environmental exposures their machinery will encounter.
Modern electric motor insulation materials include resins formulated to maintain viscosity under vacuum and bond tightly to windings. Using high-quality motor insulation materials designed for VPI processing guarantees that the final component achieves maximum mechanical durability and a longer operational lifespan.
Building reliable industrial equipment requires a processing partner with deep technical expertise. At Godfrey & Wing, we provide advanced vacuum pressure impregnation equipment and equipment servicing. Our automated systems feature deep vacuum capabilities to ensure consistent, repeatable impregnation for every cycle. Whether you process compact components or large-scale power distribution equipment, our turnkey VPI systems integrate seamlessly into your workflow to maximize throughput and eliminate defects.
Our VPI technology can elevate manufacturing quality and help protect electric motor windings against premature failure. Contact the team at Godfrey & Wing today to discuss your requirements.
Transformers are crucial components in modern power infrastructure, allowing for efficient long-distance transmission of electrical energy. As electrical infrastructure evolves to support modern smart grid transformers and renewable energy integration, transformer insulation must be able to handle increased stress and harsh conditions. Vacuum pressure impregnation (VPI) is important for improving reliability in transformers used in power transmission and distribution systems, addressing manufacturing defects that can impact performance in these settings.
Insulation breakdown typically starts with microscopic voids that are hidden deep within insulation materials. These air pockets create weak points in insulation where stress concentrates during peak operation. Environmental factors can also compound the problem, such as moisture infiltration through incomplete sealing that can degrade insulation resistance. Over time, performance issues can impact insulation performance or lead to failure.
Vacuum pressure impregnation systems remove air and moisture from transformer insulation before introducing oil or resin under extreme pressure. The deep vacuum cycle extracts air from the voids, including the microscopic spaces between tight insulation layers. Once the vacuum cycle completes, the system introduces an oil or resin under controlled conditions.
The oil or resin creates a void-free insulation system. This eliminates the specific weak points where partial discharges initiate, and the complete encapsulation prevents moisture ingress and environmental contamination.
Vacuum pressure impregnation (VPI) is especially critical for dry-type transformers that must withstand high temperatures and harsh environments. This process can lead to improved performance metrics across several areas, including:
Today’s smart grid transformers face rigorous technical demands, including the need to withstand high-frequency harmonics and rapid voltage fluctuations caused by the integration of power electronics and intermittent renewable sources. VPI dry-type transformers also need to be fire-safe and handle short-term overloads common in modern power networks.
VPI-processed units handle these modern challenges with void-free insulation. Complete void elimination provides consistent dielectric performance across the full operating range. Further, better thermal management actively extends service life, even under the frequent, aggressive load variations seen in modern infrastructure.
At The Imprex Division of Godfrey & Wing, we specialize in vacuum pressure impregnation technology for power distribution and transmission equipment. Our VPI technology combines automated process control with advanced chemistries formulated for wet and dry-type transformer insulation, for consistent results across production volumes ranging from prototype development to full-scale manufacturing.
Whether you manufacture advanced smart grid transformers or need to improve the lifespan of standard cast resin transformers, the right technology can help you achieve the process control you require. Contact us to discuss integrating The Imprex Division of Godfrey & Wing vacuum pressure impregnation systems to improve their safety and reliability.
When metal or composite parts are manufactured through casting, molding, or 3D printing, small voids (called porosity) can form within the material. These leak paths compromise a component’s ability to retain fluids or pressure, leading to quality and performance issues.
Porosity sealing is the process of filling these internal voids. The most common and effective method is vacuum impregnation, which seals pores from the inside out. This process allows manufacturers to salvage components that might otherwise be scrapped while helping to prevent failures in the field.
Porosity most often develops during solidification, when trapped gases or shrinkage create voids in the material. There are two main types of porosity:
These defects are common in die casting, investment casting, and additive manufacturing. Even when voids are not visible on the surface, they can lead to leaks, corrosion, and cosmetic flaws. Problems frequently emerge after surface finishing, when coatings such as plating, paint, or powder coat blister or fail to adhere due to moisture or air inside the pores.
At Godfrey & Wing, porosity sealing is achieved through vacuum impregnation. The process begins by placing the part in a sealed chamber. A vacuum is applied to remove air from the internal pores, creating space for sealant. The sealant is then introduced under pressure, fully penetrating the voids. Afterward, the part is removed and the sealant is cured, forming a permanent, impermeable barrier.
This method effectively seals both blind and through porosity without altering the part’s dimensions or material properties. Because the process preserves structural integrity, manufacturers can reliably salvage high-value parts rather than discarding them.
Porosity sealing provides a range of key benefits, including:
By addressing porosity early, manufacturers safeguard product quality, customer trust, and profitability.
Porosity sealing is essential for eliminating porosity in cast, molded, or 3D-printed parts. As a global leader in this technology, Godfrey & Wing provides vacuum impregnation services and systems trusted by top OEMs in automotive, aerospace, medical, and energy sectors.
We offer flexible solutions, from stand-alone systems to fully automated production-line integration, backed by unmatched reliability and technical expertise. With more than seven decades of industry experience and a commitment to continual improvement, we help manufacturers meet the most demanding performance standards. At Godfrey & Wing, we don’t make your bad castings good; we make your good castings better.
Contact us today to discuss your porosity challenges.
When 3D printing was first developed in the 1980s, it was primarily used for proof-of-concept models or initial prototypes. Early limitations in technology and materials meant that 3D-printed parts were rarely suitable for field testing or production. However, the past decade has brought rapid advancements in additive manufacturing. These advancements have allowed for more sophisticated materials, faster product development, customization, and greater design freedom.
Modern-day 3D printing has streamlined product development cycles and design iterations. In sectors like die casting, 3D printing is often used to test working models for fit and function before full-scale production begins. The technology helps die casters bypass the costly and time-consuming aspects of creating and testing dies.
However, parts created through 3D printing are susceptible to the same porosity that plagues those created through more traditional processes. Porosity is inherent in the properties of the material and technology. These tiny voids or imperfections can weaken parts and lead to leaks. Although porosity may not be fully eliminated within the 3D print process itself, it can be effectively sealed through vacuum impregnation.
This guide will discuss how vacuum impregnation solves porosity issues in 3D-printed parts, reveal common applications for vacuum impregnation, and clarify misconceptions about the process.
Porosity refers to microscopic voids or defects that form during the 3D printing process. These occur due to incomplete fusion between material layers or trapped gases during melting and solidification. In metal additive manufacturing, such as laser powder bed fusion (LPBF), porosity can seriously compromise mechanical integrity.
There are two primary types of porosity:
In addition to reducing the durability of 3D-printed parts, these voids can make components unsuitable for pressure-sensitive or high-performance applications. Porosity can also affect surface finish and dimensional accuracy.
In applications that require pressure-tight parts, even microscopic leak paths can cause catastrophic failure in the field. Moreover, certain industries, such as aerospace and medical devices, maintain strict quality control standards that do not accept hidden defects. In these industries, knowing how to seal 3D-printed parts effectively is critical.
Vacuum impregnation is a proven solution for sealing porosity within 3D-printed components. The process involves placing the part in a vacuum chamber and introducing a liquid resin or sealant that fills micro-voids inside the material. As the sealant cures, it bonds within the part’s internal structure. The process of vacuum impregnation has been shown to significantly improve multiple aspects of 3D prints, including the following:
All of these benefits are what make vacuum impregnation ideal for functional prototypes, end-use parts, and any other application where consistent performance is critical. Proper resin selection, vacuum pressure control, and curing time are essential for ensuring full impregnation and maximizing part performance.
Two common material types that benefit from vacuum impregnation include:
In addition to increasing strength in 3D-printed parts, vacuum impregnation contributes to sustainability. By sealing internal defects, manufacturers can reduce scrap rates and extend the useful life of parts, which minimizes material waste and energy consumption during production. This makes vacuum impregnation an environmentally responsible post-processing method that aligns with green manufacturing principles.
Here are the main reasons for sealing 3D-printed parts via vacuum impregnation.
Even highly optimized 3D-printed parts typically achieve a density of about 98-99%. That remaining 1-2% of micro-voids is enough to cause fluid or gas leaks. For applications requiring airtight or watertight performance, such as aerospace components, cooling channels, or sensor housings, sealing this porosity is essential.
Because 3D-printed parts aren’t as dense as machined parts, they often lack comparable strength. Vacuum impregnation reinforces these parts by bonding internal layers and increasing structural density. As the sealant cures, it enhances layer adhesion and contributes to a more robust part.
Blooming is a condition where the 3D-printed part swells as layers absorb fluids. This not only affects visual appearance but can degrade performance. Vacuum impregnation eliminates this risk by filling the voids where fluid would otherwise accumulate.
In addition to improving performance, vacuum impregnation can increase confidence in the manufacturing process. Engineers can validate prototype designs knowing that material limitations, such as porosity, can be managed effectively. This shortens the timeline between prototyping and production, saving development time and costs.
Several misconceptions persist about vacuum impregnation in 3D printing. Let’s go through them.
No. Build lines result from the layer-by-layer deposition of material and are part of the surface texture. Build lines are only a concern if the part is intended for cosmetic applications. Vacuum impregnation addresses subsurface porosity, not surface appearance.
No. Surface cracks or cosmetic flaws aren’t sealed because vacuum impregnation works within the material structure. Only the impregnation sealant that has been drawn into the walls by the force of the vacuum and pressure remains in the part. For visual defects, other post-processing methods like sanding or coating are more suitable.
No. The process occurs below the surface and does not affect the part’s external dimensions. This makes it suitable for precision applications where tight tolerances are required. Vacuum impregnation is designed to integrate seamlessly into existing workflows. The process is non-destructive and can be automated for high-volume production, making it ideal for industries looking to scale 3D printing without compromising quality.
Established in 1948, Godfrey & Wing is the world’s longest-serving and largest provider of vacuum impregnation services, equipment, and sealants. With a legacy of innovation and precision, we help manufacturers across industries enhance the performance and reliability of their components, 3D-printed and otherwise.
We work closely with engineers and manufacturers to develop tailored solutions for their applications. Whether your priority is sealing micro-porosity in functional prototypes or reinforcing structural integrity in final-use parts, our team can help you implement vacuum impregnation with minimal operational disruption and maximum results.
Whether you’re prototyping a new part or preparing for scaled production, sealing with vacuum impregnation ensures your parts meet the highest standards of strength and reliability. To learn more about our process or to get started on your solution, contact us today.
Porosity is any void or hole in, or on, a casting and is caused by gas formation or solidification shrinkage that occurs while the metal solidifies. If the casting needs to be pressure tight, porosity can allow gas and fluids to seep from the part. In this blog, we will discuss the difference between gas and shrink porosity and the best solution to seal porosity.
One of the most prevalent types of die casting defects is gas porosity, which occurs when rounded air pockets or voids form within or on the surface of the casting. While minor levels of porosity may be allowable for non-critical parts, gas entrapment can ultimately compromise the quality and integrity of critical parts for high-strength applications. Because of this, manufacturers must detect and address porosity promptly in adherence with industry standards.
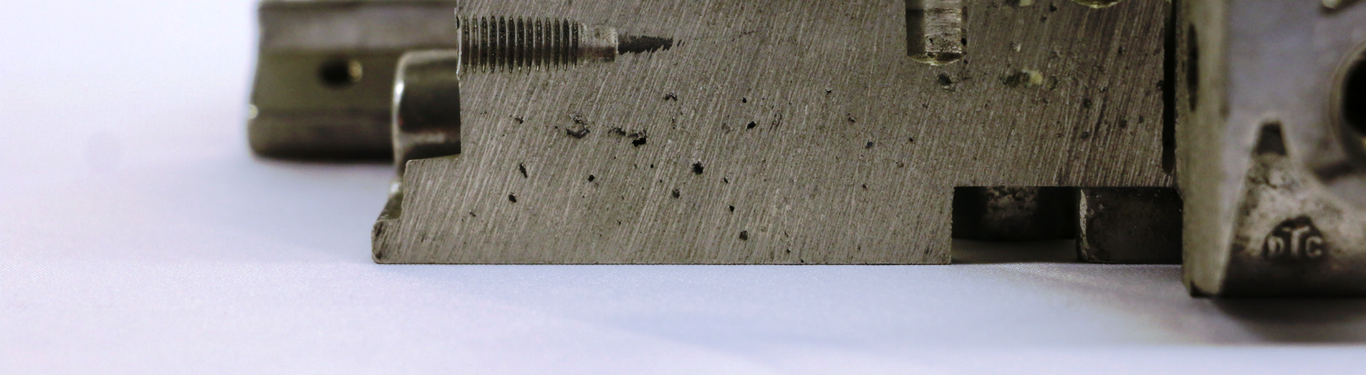
There are several different types of gas porosity defects. These include:
Shrinkage porosity defects are cavities that form when a casting solidifies inside the tool, but there isn’t enough liquid metal to fill the newly formed voids. These have angular surfaces and are different from air entrapment holes, which have rounded shapes.
Shrinkage porosity can cause material weakening. If on the surface, this porosity can lead to lower corrosion resistance as well as a worsened aesthetic appearance. Identifying the size, shape, and position of cavities is essential to determine which defect is occurring and what is causing it to occur.
There are several different types of shrinkage porosity defects, including:
As the amount of porosity increases in an aluminum or iron casting, it can become interconnected and create a leak path. The porosity makes the casting unusable for holding pressure in applications like pumps, compressors, transmissions, and plumbing fixtures.
The most economical and successful approach to stop casting porosity is through vacuum impregnation. Vacuum impregnation is a method that seals the casting. To complete this process, the impregnating sealant is introduced into the voids within the wall thickness of the casting through vacuum and/or pressure methods.
This method is a cost-effective and permanent solution to casting porosity. Additionally, there is no limit to the size of castings that can be impregnated. Since the impregnation process occurs within the part, it will not distort, discolor, or affect the casting.
With first-time-through (FTT) recovery rates of over 99%, Godfrey & Wing’s vacuum impregnation equipment provides an effective and economical solution for stopping casting porosity. We build our systems around OEM’s parts sealing requirements to ensure leak-free and pressure-tight casting.
Die casting is a metal casting process that involves injecting molten metal into a die using high pressure. Die casting facilitates the production of hundreds or thousands of pieces with high dimensional accuracy and a good surface finish, making it highly economical; however, maintaining quality and consistency at such high volumes comes with its own challenges. Manufacturers need to account for porosity, or the tendency for die castings to have voids or holes that cause surface-level flaws. Read on to learn more about die casting porosity, problems it can cause, and how vacuum impregnation seals die casting porosity.
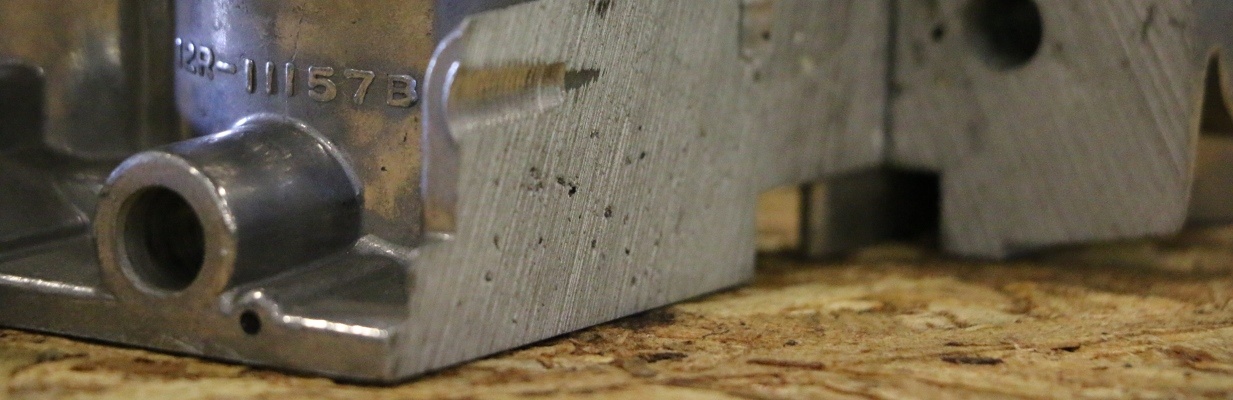
Die casting porosity refers to specific defects found within the casting. Two of the most common types of porosity in completed metal goods are gas porosity and shrinkage porosity. Gas porosity is often caused by trapped air or other gases during solidification. It is always buoyant, meaning the resulting bubbles are typically found near the top of the casting (as seen below).

Shrinkage porosity, on the other hand, refers to internal voids that can form as the metal cools. This is because the solid metal volume is less than the volume of liquid metal at higher temperatures. Shrinkage porosity has a linear or jagged appearance and tends to occur in either the drag or cope portion of the casting (below the surface).

In addition to the above, having too much die lube can also contribute to porosity in die casting. While die lube is essential for removing cooled goods from the molds, too much can interfere with solid formation and create surface-level flaws.
While porosity is inherent in die casting manufacturing, it can impact part performance, especially in applications where pressure integrity is a vital characteristic. Far from just being an aesthetic or durability problem, die-cast porosity can lead to early breakdowns or even failures. Consider the following examples:
Blind porosity creates gaps that sit along the surface, pushing slightly into the interior but not creating uninterrupted passages for liquid to seep in. Manufacturers can expose blind porosity during the finishing stages. While it doesn’t make goods mechanically weaker, it does increase the risk of corrosion. The pores can also hold onto cleaning chemicals from powder coating or anodizing pre-treatments and then leach out after treatment, causing blemishes on the surface.
Through porosity creates a leak path that runs through casting walls, or can be exposed after machining. This can weaken the metal and make it unsuitable for applications that require excellent pressure tightness, such as automotive and marine applications. Through porosity may make components weaker, create failure points, and prevent parts from reliably holding fluids.
These pores are completely enclosed and don’t create leak paths. However, fully enclosed pores can become problematic if they’re exposed during surface finishing.
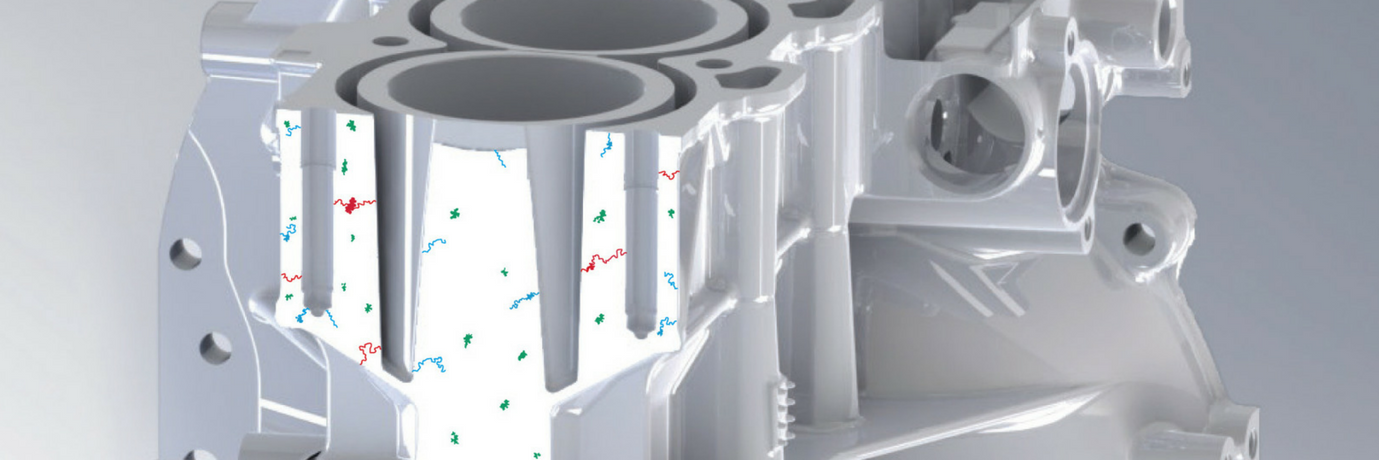
Manufacturers can significantly reduce or completely eliminate failures due to die casting porosity with the right equipment and processes. One of the most effective methods is vacuum impregnation. With this controlled method, manufacturers use vacuuming and pressure to introduce the impregnating material into the voids, sealing the voids to make the casting fit for pressure-sensitive applications.
Benefits of using die casting vacuum impregnation include:
Manufacturers can use vacuum impregnation for castings of any size, creating a permanent seal as well as a more consistent look, feel, and functionality in finished products.
At Godfrey & Wing, we specialize in closing the gaps left by die casting processes. Our equipment can provide fast, cost-efficient, and thorough vacuum impregnation processes to address porosity in die casting manufacturing. We’re committed to building systems that create effective, reliable seals that meet or exceed OEM requirements, and our team has decades of experience researching and improving solutions for die cast porosity.
Contact us today to learn more about our products and services.