YOUR CART
- No products in the cart.
In order to maintain impregnation sealant for optimal performance, there are two vital tests that should be performed on a regular basis:
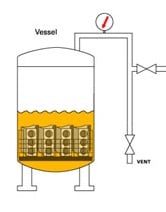
Fundamentally, there are two factors that control impregnation results – sealant quality (formulation and working condition) and vacuum (depth of vacuum). Because vacuum is such a critical factor in achieving superior results, a Godfrey & Wing representative will always recommend a DV (or DVP) process over WV when discussing the impregnation of High Value parts.
A common question asked by customers is “Why do aluminum castings discolor during vacuum impregnation?”. Aluminum parts with highly machined surfaces are more likely to be affected than those that are cast.
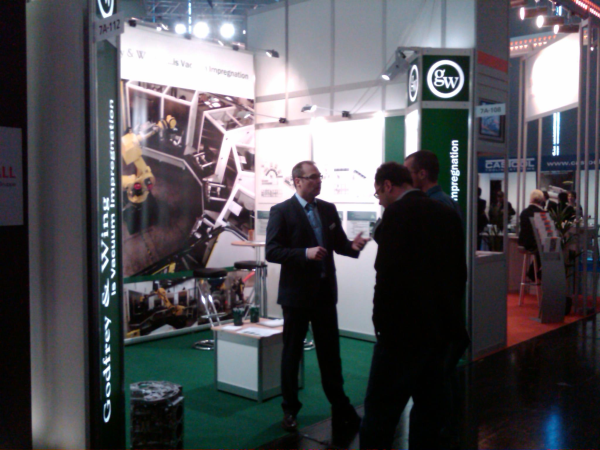
This year’s EUROGUSS attracted a record number of domestic and foreign visitors to Nuremberg as 8,200 people were looking for information about die casting foundries and foundry suppliers. The 383 exhibitors, of which 42% were international companies, did not just make contacts – many took orders. A wide range of products were represented from die castings, materials, furnaces, die casting machines and moulds to after treatment, quality control and research and development.
Technology, Processes & Products
Why does GW recommend the dry vacuum and pressure (DVP) process?
In order to help determine what size vacuum impregnation system you need, there are a few questions you should answer first. The goal is to determine the total volumes and size of the parts that need to be impregnated and how that fits into your existing manufacturing schedule.