YOUR CART
- No products in the cart.
One of the most common questions in vacuum impregnation is how much does it cost to impregnate a part, or in other words, how much sealant will a part consume? Parts consume sealant in two ways as part of the normal vacuum impregnation cycle.
The first way that parts consume sealant is that sealant actually penetrates and gets trapped inside the part where the sealant then solidifies and seals the part. The second way sealant is consumed in the vacuum impregnation process is the design waste. This is the excess sealant on the outside of the part that ultimately gets washed off and discarded. If you know the amount of sealant that gets trapped (picked up) inside the part during the impregnation cycle, then you can do a rough estimate of the overall cost simply by multiplying the “pick up” amount by 4.
This calculation not only takes into consideration the sealant cost but also compensates for compressed air, electricity, water, labor, and design waste associated with the overall vacuum impregnation process. It does not, however, include any factor for profit, depreciation, freight, general or administrative expenses, selling costs, or any other non-impregnation process costs.
With that in mind, we can provide some basic information to help you establish sealant pick up rates for both powder metal (PM) parts and traditional aluminum-based parts. This information is based on historical data and is only meant to provide a ballpark understanding of typical sealant consumption. Given that every part is unique and different your application may or may not adhere to these guidelines. As for PM parts with a typical density of 6.8, you can assume an average pick up rate of 1 gram of sealant for every 40 grams of compacted metal. So, if a compacted part weighs 160 grams it will usually pick up about 4 grams of sealant.
For aluminum, let’s assume a density of 2.8 grams/milliliter. If you know the weight of the aluminum part in grams you can simply divide that by the density to get the volume of the part in milliliters. By dividing that by 1,000 you can convert the volume to liters. Once you have the volume you can simply multiply that result by a factor of 8 to get the estimated sealant pick up. For example, if a part made from aluminum weighs 1,500 grams, divide that by 2.8 to get 535mL. Divide 535 by 1,000 to convert to liters which will yield .535. Multiplying the .535 by 8 will provide an estimated sealant pick up of 4.3 grams. This information can then be used to help establish your annual sealant volume or daily sealant consumption.
As we begin a New Year, we want to share our top 5 blog posts of 2012. If you missed any of these articles, be sure to check them out. They include helpful information about vacuum impregnation processes, equipment and maintenance.
In an earlier blog article, we discussed the most common ways that sealant can get into vacuum pumps during the impregnation process.As a reminder, the list included:
The next step is to discuss how to defend against the problem of sealant getting into vacuum pumps. Even if an impregnation system is properly set up and maintained, accidents can happen that can lead to this problem. The best defense is a trap that the sealant can be “caught” in prior to reaching the pump.
Depending on the level of protection desired, traps can be as simple as a loop in the vacuum hose/line or as sophisticated as a mechanical trap with sensors.These traps are located between the impregnation vessel and the vacuum pump.The purpose of a trap is to give the sealant an alternative place to go (get trapped) versus into the vacuum pump.
The simplest approach, which is effective when sealant rarely enters the vacuum pump, is to loop the vacuum hose/line in such a way that gravity alone stops sealant before the pump.In this case, the weight of the sealant cannot overcome gravity and therefore cannot reach the peak of the vacuum hose, thereby “trapping” it in the line, typically to drain back into the vessel.
The next level of technology is a mechanical trap that is either maintained manually or set up for semi-automation (Fig 2 below). With these types of traps, there is a level sensor that sends a signal to the PLC, indicating that it is full and needs to be drained. A manual drain at the bottom allows maintenance personnel to easily drain the system.
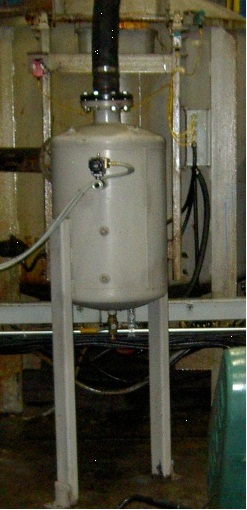
The highest level of technology is a fully automated trap that allows for continuous running of the impregnation system (Fig 3 below). These traps also have level sensors to indicate when they are full. In addition, the traps are connected to pneumatic valves that are programmed to open between cycles, draining any sealant in the trap back into the sealant reservoir.
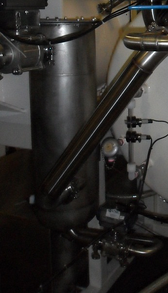
The interior of the mechanical traps can be of various design. Those requiring the least maintenance will have steel baffles that the air/sealant would have to navigate to get to the pump. Designed correctly, these are very effective and pulling any sealant out of the air flow.
Another option is to have filter elements (typically in the 5 micron range) that the air can pass through, yet the sealant will be trapped in.
Depending on the size and performance of the system, a cost-effective Vacuum Sealant Trap can be designed and installed. The additional protection for the vacuum pumps are worth the investment so as to reduce downtime and maintenance costs.
For more information on this topic, contact Godfrey & Wing.
Vacuum impregnation seals the porosity in metal castings, thus making leaky castings pressure tight. But how exactly does it work? The following demonstrates the 4 steps to the vacuum impregnation process. (more…)
There are a couple of possibilities that would require a double cycle impregnation.
 The other morning I was walking the dog around 5:00 AM, and I noticed how exceptionally crisp and brilliant the stars were in the pre dawn sky, shining though the high pressure system overhead. While finishing the walk around the neighborhood, I thought about mankind’s worldview that the earth was flat as recent as 600 years ago and the reluctance of decision makers of that time, influenced by the rhetoric of naysayers, to accept anything other than the status quo.
Did we make money on that job?
A common problem for those operating impregnation systems is sealant making its way into a vacuum pump. Sealant inside a pump (Figure 1) will lead to increased maintenance costs; premature pump rebuilds; or early pump replacement resulting from irreparable pump damage. There are multiple ways sealant can end up in the pump.